Do not treat every line as the same failure
A surface can show polishing, abrasion, scoring or transferred material. These descriptions are useful because they describe what is present, but they do not establish an acceptable condition. A visually small mark can matter if it affects a critical precision surface.
A competent inspection should identify the location, orientation and extent of the damage. The component may require dimensional and surface assessment beyond what a photograph can show. Do not invent a permissible scratch depth or assume that a fingernail test replaces the actual service criteria.
Understand why the mating part matters
Abrasion can involve hard particles interacting with surfaces, while adhesive damage involves material interaction and transfer at contacting surfaces. The resulting debris and damaged geometry can affect both sides of the sliding pair. The original source may also be outside that pair.
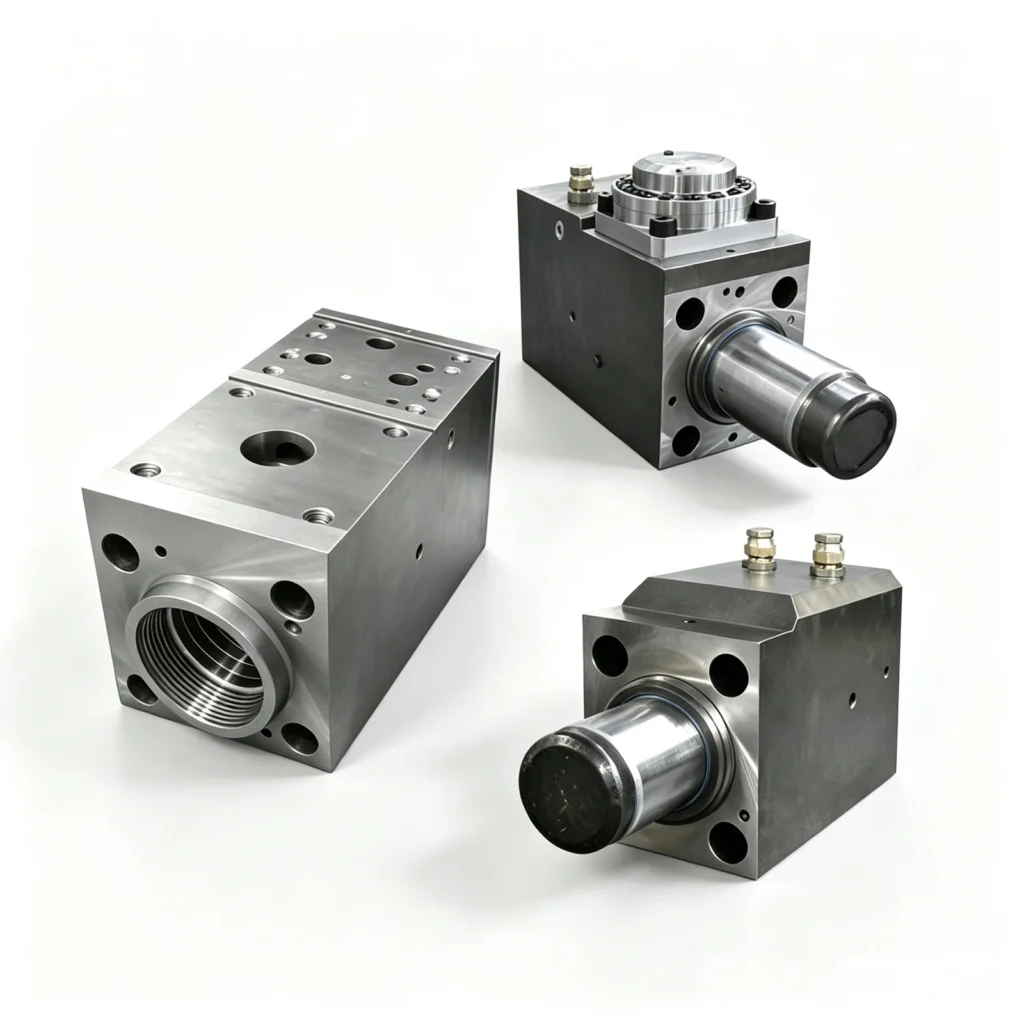
The piston therefore needs assessment whenever cylinder damage is reviewed. Its condition, geometry and compatibility may influence the replacement decision. A new cylinder is not a complete repair if a damaged or incorrect piston is returned to it.
| Finding | Inspection implication |
|---|---|
| Scoring in the bore | Assess location, dimensions and corresponding piston surface |
| Transferred or torn material | Review both contacting surfaces and seizure history |
| Debris or contaminated oil | Investigate source and required system clean-up |
| Repeated damage after replacement | Recheck fit, assembly and operating conditions |
| Unknown previous rework | Establish actual geometry and approved repair status |
Separate reconditioning from cosmetic improvement
Polishing or removing material changes the surface and potentially its dimensions. That can alter the intended fit and any treated surface condition. A bore that appears smoother after hand rework has not necessarily become serviceable.
Any honing, grinding or other reconditioning needs an approved method and acceptance criteria for the exact component. If those do not permit a repair, replacement is the appropriate scope to evaluate. Do not use a generic abrasive procedure to make a new piston enter a damaged cylinder.
A practical warning is a bore that has already been polished during an earlier repair but has no record of the final dimensions or method. Its appearance cannot establish the original fit, and copying a measurement from one remaining unworn area may not resolve the uncertainty. The assessment must determine what geometry and surface condition remain acceptable for the intended assembly. A replacement decision based on that finding is stronger than one based only on whether the piston can move by hand.
Close the cause before the replacement is fitted
Review the fluid findings, relevant operating conditions and assembly history so that the repair addresses more than the visible mark. Where contamination is involved, the connected system may require a defined corrective process before fresh precision components are installed.
For NEWLAND supply, identify whether the requirement is a cylinder, piston or a specified combined assembly, with the relevant references and revision. Include the technician’s acceptance decision for retained components. The final repair should leave a documented compatible assembly and a completed return-to-service check, rather than just a list of new parts.
Related products and guides
Hydraulic Breaker Cylinders
Hydraulic Breaker Piston Damage: Chipping, Seizure and Replacement Scope
Hydraulic Breaker Oil Contamination: Milky Oil, Debris and the Inspection Record
Hydraulic Breaker Pistons
Matching a Hydraulic Breaker Piston: Why Diameter Alone Is Not Enough